
The problem that starts on the plant floor
Premature gelation under thermal swings is the sort of trouble that eats production quotas and patience in equal measure. In many presses and impregnation lines, a thermoset batch will behave fine at 120°C and then clump at 150°C, shortening gel time to minutes and spawning rejects. The fix often lies not in brute heating or hurried cures, but in the resin chemistry — hence the growing interest in rosin resin modifications of phenolic formulations. In County Wicklow trials, operators noticed that modified mixes tolerated repeated 150°C cycles far better than neat phenolics, which gives a practical anchor to theory and practice.
Why rosin modification matters: polymer mechanics in plain speech
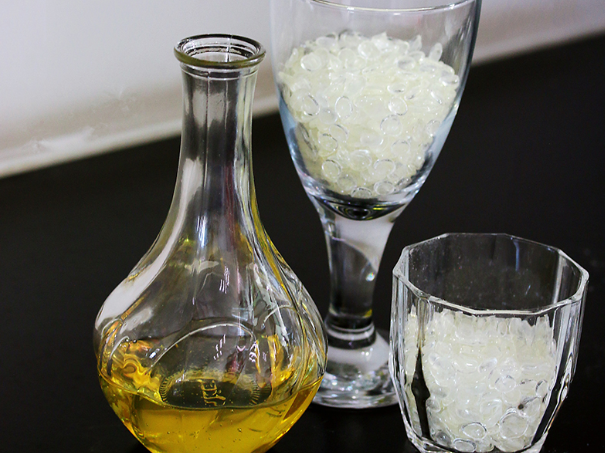
Rosin-modified phenolic resin brings two practical advantages: it tempers crosslink density and adjusts viscosity so gel time becomes predictable rather than capricious. Phenolic resin alone can crosslink fast when local hotspots appear; adding rosin derivatives introduces flexible aliphatic segments that slow network formation. That tempering reduces thermal sensitivity without wrecking heat resistance — the resin still behaves as a thermoset, but it resists forming an irreversible gel the moment a platen spikes to 150°C. In short, you get stability where you used to get chaos.
Common mistakes and what the floor teaches you
People often exacerbate gel issues by chasing cure speed: raise temperature, shorten residence, repeat. That compounds uneven crosslinking and raises reject rates. Another frequent error is ignoring raw-material variability — rosin batches from different suppliers (or different pine harvests) vary in acidity and softening point, which changes how they modify phenolics. Check supply certificates and, where possible, sample blends from each shipment. A sensible lab run will flag a drift in gel time before a whole shift does.
Operational production teardown
Here’s a concise teardown of controls that help: measure resin viscosity at ambient and at process-relevant temperatures; monitor pot life and gel time in minutes using the same cure profile the line uses; and map thermal uniformity across tooling. In this section I’ll use {main_keyword} and {variation_keyword} as placeholders to remind engineers to lock down their process-specific terms early in scale-up. Keep a short log: resin lot, measured viscosity, pot life, and bench gel time at 150°C. That traceability prevents surprises once the batch hits the press.
Alternatives and trade-offs
If rosin modification feels unsuitable, alternatives include novolac formulations with adjusted catalysis or epoxy-phenolic hybrids that trade some thermal endurance for slower gel kinetics. Each choice trades durability, cost and adhesive behaviour — and none absolve you from controlling thermal ramps and dwell times. For small runs, adjust your cure schedule; for volume, standardise on a resin system that tolerates the 150°C ceiling. Also remember the source: genuine pine tree resin characteristics will influence how a rosin additive behaves in your matrix.
Practical checks before you sign off a run
Run three simple, repeatable checks: 1) bench gel time at the intended 150°C profile; 2) viscosity sweep to detect shear-thinning or thickening trends; 3) a short-cycle press test that mirrors the slowest point on your line. These aren’t exotic tests — they’re basic diagnostics that separate a batch that’ll behave from one that won’t. Attend to them before you call any batch “production ready.”
Advisory: three golden rules for curing chaos into consistency
First: control thermal uniformity — uneven tooling causes local gel hotspots, so get the heating map and correct it. Second: standardise resin input — every rosin lot needs verification against a narrow viscosity and acid-number band. Third: prioritise bench gel time measured under the exact ramp-and-hold profile used on the line. These metrics tell you whether a formulation will tolerate 150°C or toss out rejects. Keep records; they become the recipe for repeatability.
Production realities are stubborn, but so are good materials and good practice — the right rosin-modified phenolic approach stops gel time from being a mystery and turns 150°C from a day of dread into a predictable step. — KOMO