
Introduction
You’re walking a busy showroom in Guangzhou, samples everywhere, timelines tight. End table manufacturers are counting weeks, not days, and the next season is already calling. Last quarter, 37% of SKU delays traced back to component inconsistency and rework, from edge banding scuffs to late powder coating runs—kweli, it stings. So, how do you decide when to build in-house and when to partner outside, without blowing cost, quality, or speed? (And without stressing your team.) Is there a clear, practical way to choose the right path for each design and quantity?
This guide shares a grounded comparison for your line planning. We keep it pole pole, but precise. You’ll see the hidden traps, the new levers, and why a small process tweak can save big on lead time. Let’s move to the deeper layer and map what’s really driving risk and return.
Hidden Friction in the Wholesale End Table Play
Where do costs hide?
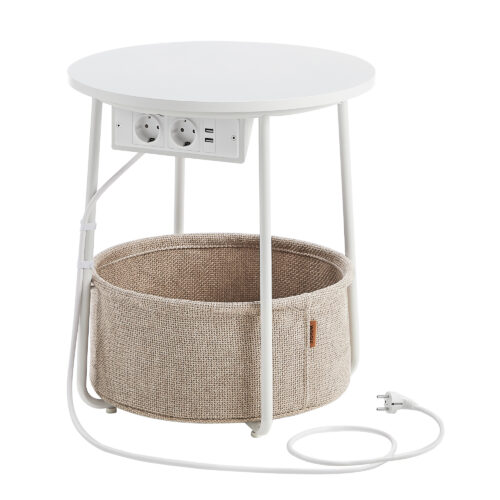
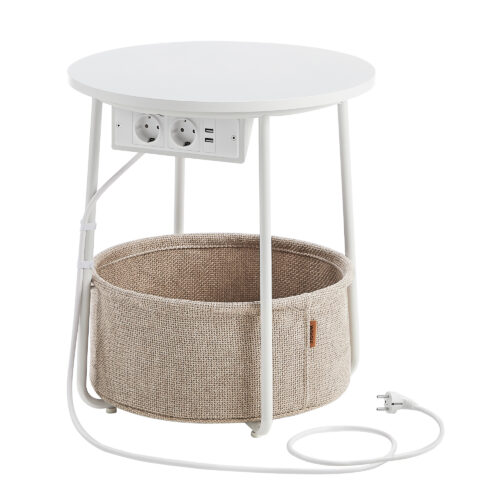
Many teams lean on a wholesale end table route to smooth capacity peaks. On paper, it’s fine: stable supply, set MOQ, clear unit cost. In practice, the “easy” choice can mask tricky friction. Technical? Yes. The bill of materials shifts once you add charging modules or power converters. That means new QC sampling protocols, extra packaging tests, and sometimes a revised certification plan for a simple side table—funny how that works, right? Even the finish stack matters; a thin primer under powder coating can create color drift across batches, which then reads as a different sheen under retail lights.
Traditional purchasing also hides soft costs. Communication loops add days, especially when CNC routing updates or hardware swaps happen late. When tolerance notes live in chat threads (sawa, we’ve all done it), you pay later in rework. Freight consolidations slip. Edge banding pulls at tight radii during humid transits. Look, it’s simpler than you think: the flaw isn’t the wholesale model, it’s the assumption that “standard” equals “stable.” If your line mixes veneer, solid wood, and metal frames, the tolerance stack-up shifts batch to batch. Without documented first-article approval and a clean change log, you chase the problem instead of controlling it. That’s the hidden tax many teams accept.
The Next Wave: Smarter Specs, Leaner Decisions
What’s Next
Forward-looking teams aren’t just choosing a vendor. They are adopting new technology principles to make the choice measurable. First, parametric spec sheets cut ambiguity. You lock key tolerances, define fastener families, and set finish delta-E limits, then plug them into your ERP so each revision is traceable. Second, digital twins for your top movers (yes, even a humble C-table) simulate stress on brackets and leg joints, so you pick hardware that survives real-world wobble before the first jig is cut. Third, modularity is your friend: standardized feet, shared chargers, and common screws reduce SKU chaos and protect lead time during supply spikes.
In this model, your end table supplier becomes part of a controlled system, not a black box. You compare “build vs. buy” with clear inputs: takt time for your CNC cell, coating booth capacity, and a living cost model that updates with freight and carton changes. Semi-formal, yes—but the payoff is real. You prevent rework by catching variance at the drawing level. You focus your factory on items where your fixturing shines and outsource pieces where a partner’s automated welding or UV-cured lacquer line wins. The result is fewer rush jobs, cleaner QA gates, and steadier on-time rates—small win, big peace.
How to Decide: A Short List That Works
Here’s an advisory checklist to keep your balance smart and steady:
1) Variance Risk Score: Rate each design by tolerance sensitivity, finish complexity, and hardware risk. Include joinery type, veneer cut, and bracket torque. If the score is high, demand first-article approval with retained samples and tighter QC sampling. If low, wholesale can flow.
2) Capacity Fit Index: Map cycle time for your CNC milling, sanding, and coating cells. If the model spikes above 85% utilization during peak orders, outsource modules that carry the longest curing or setup times. Keep your line for SKUs where fixturing gives repeatability.
3) Total Landed Cost Window: Model carton strength, cube, and freight tiers alongside MOQ and rework potential. Don’t forget packaging inserts, corner guards, and drop-test deltas. If your spread swings more than 8% with minor spec shifts, lock modular components to stabilize.
Evaluate with discipline, but stay human about it—teams need breathing room to do good work. When you align specs, capacity, and cost windows, your end tables ship on time and look the same in every store. That’s the goal, si ndio? For more grounded practices and partnership options that fit this approach, see SONGMICS HOME B2B.