
Introduction: A Short Shop-Floor Moment That Changed My View
I was standing by a production run when a simple tool offset error stopped the line for an hour. I remember the hum, the flicker of alarms, and the tension on every face — that moment made me question our choices. In the next breath I looked up numbers: 5 axis machining center manufacturers are pushing new models every quarter, yet adoption gaps remain (supply chains, training, and desktop confusion included).
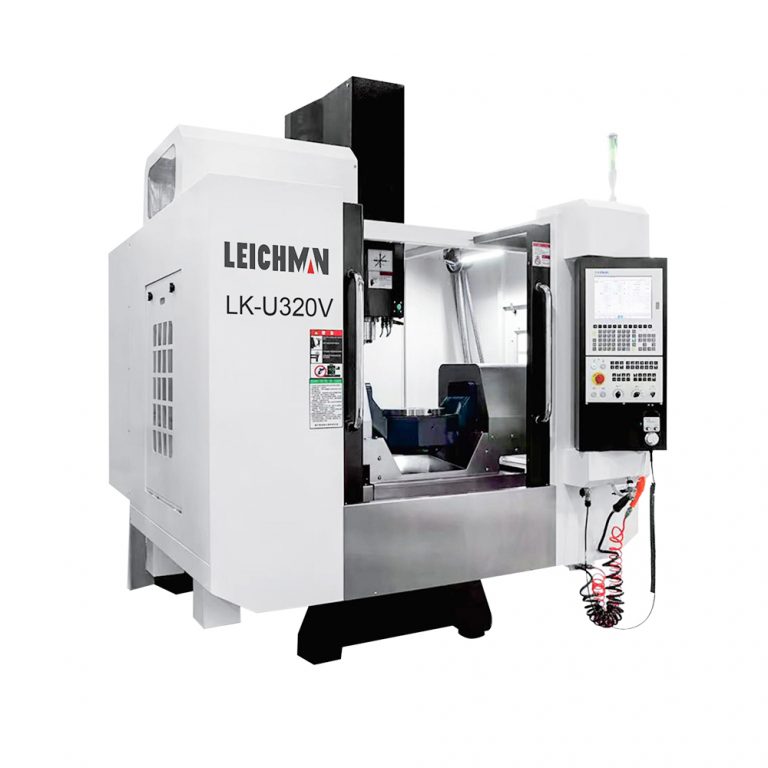
Data shows shops upgrading to five-axis systems often expect 30–50% cycle time gains. So why do so many teams still struggle after installation? I want to help you cut through the marketing noise and practical headaches. We’ll unpack what really trips teams up, how to spot the quirks, and what to ask next — practical moves you can act on tomorrow. Let’s dig in.
Part 2 — The Hidden Flaws: Why Traditional Solutions Leave Users Frustrated
multi spindle cnc machining center sounds like the quick fix: more tools, more spindles, faster output. In my experience, that glance over the spec sheet misses core pain points. Traditional setups assume flawless programming, perfect fixtures, and endless operator patience. In reality, broken assumptions show up as repeated downtime and poor first-article quality. I’ve seen shops where inconsistent spindle speed and incorrect feed rate settings doubled scrap on complex parts. It’s not just the machine — it’s the whole workflow.
Look, it’s simpler than you think: the tool changer may be rated for high-cycle work, but if your tool offsets and G-code are sloppy, you’ll still have crashes. Tool library errors. Fixture shimming. Operator fatigue. Those are the small defeats that add up. We lost time because the coolant system was underspecified, and worse, the CNC controller wasn’t set up for layered compensation — sad, but fixable. — funny how that works, right? My point: manufacturers can deliver hardware, but the support for real-world integration (training, post-processing, setup recipes) often lags. That’s the gap I learned to look for first.
So what breaks most often?
In short: mismatch between capability and process. Big spindle torque doesn’t help if your fixturing is weak. High rpm is useless without tuned feed rate. I recommend auditing the whole chain: tooling, fixture design, post-processor, and operator competence. I do it myself now when evaluating a new line — and it saves headaches later.
Part 3 — What’s Next: Principles for Better Adoption and Clear Metrics
Now let’s shift forward. I want to outline practical principles that actually ease the transition to advanced machining. New systems must be matched to process, not wishful forecasting. Start with modular testing: validate a single part on a candidate machine before scaling. Consider edge computing nodes for real-time telemetry if you plan to monitor spindle load, and check power converters and coolant system capacity against peak demands. These are not buzzwords; they are the plumbing that makes consistent parts possible.
For shops looking at service bundles, try multi spindle cnc machining services early in the procurement process — they can show you realistic cycle times and maintenance windows. In my experience, pilot runs uncover fixture issues and G-code quirks you won’t see on paper. Also, ask vendors for clear post-processing support and a training plan that puts operators at the center. — small wins stack into big gains.
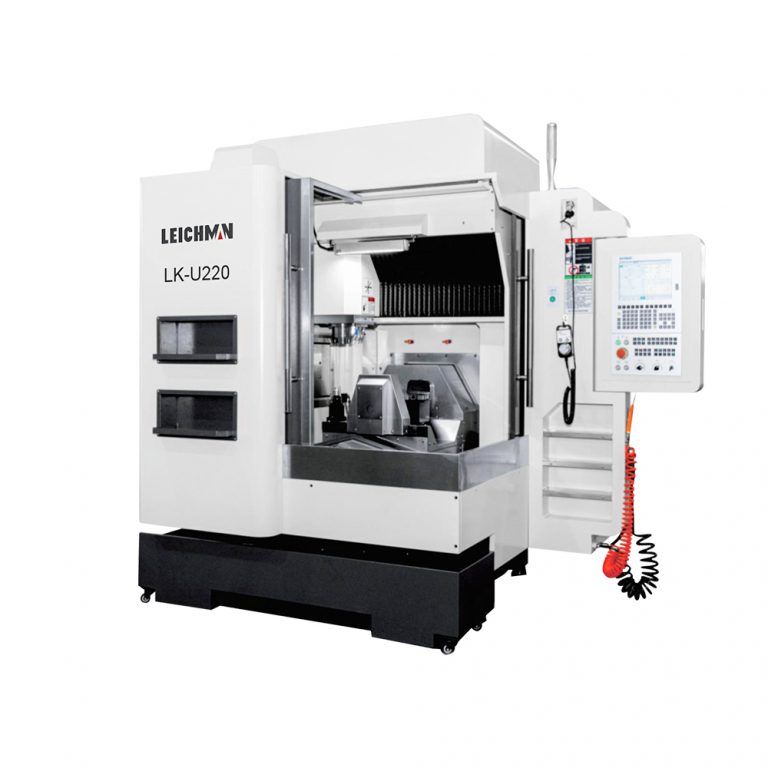
What metrics should you use?
Here are three evaluation metrics I use when comparing solutions:- First-pass yield: the percent of parts that meet spec without rework. It tells you about integration quality.- Mean time between failures (MTBF): how often production halts due to machine issues.- Total cost per part (including tooling and setup): this reveals the true ROI beyond cycle time numbers.
Use these to compare apples to apples. Ask for measured data from comparable parts, not just idealized run charts. I’ve learned that numbers matter — but context matters more. Evaluate with both head and gut. In the end, the right partner is the one who helps you improve those three metrics steadily, not just sell a high-rpm spec sheet. To explore machines and support that match these principles, check Leichman for options and case references.