
Introduction
I remember standing on a factory floor where a single jam shut down three production cells for an hour—costly, frustrating, and all too common. In that plant, wet wipe machinery accounted for 60% of downtime costs that quarter, and the finance team was clear: small faults add up fast. Wet wipe machinery, after all, must balance speed, hygiene, and consistent sealing under tight margins. (We tracked torque readings and cycle times that week.)
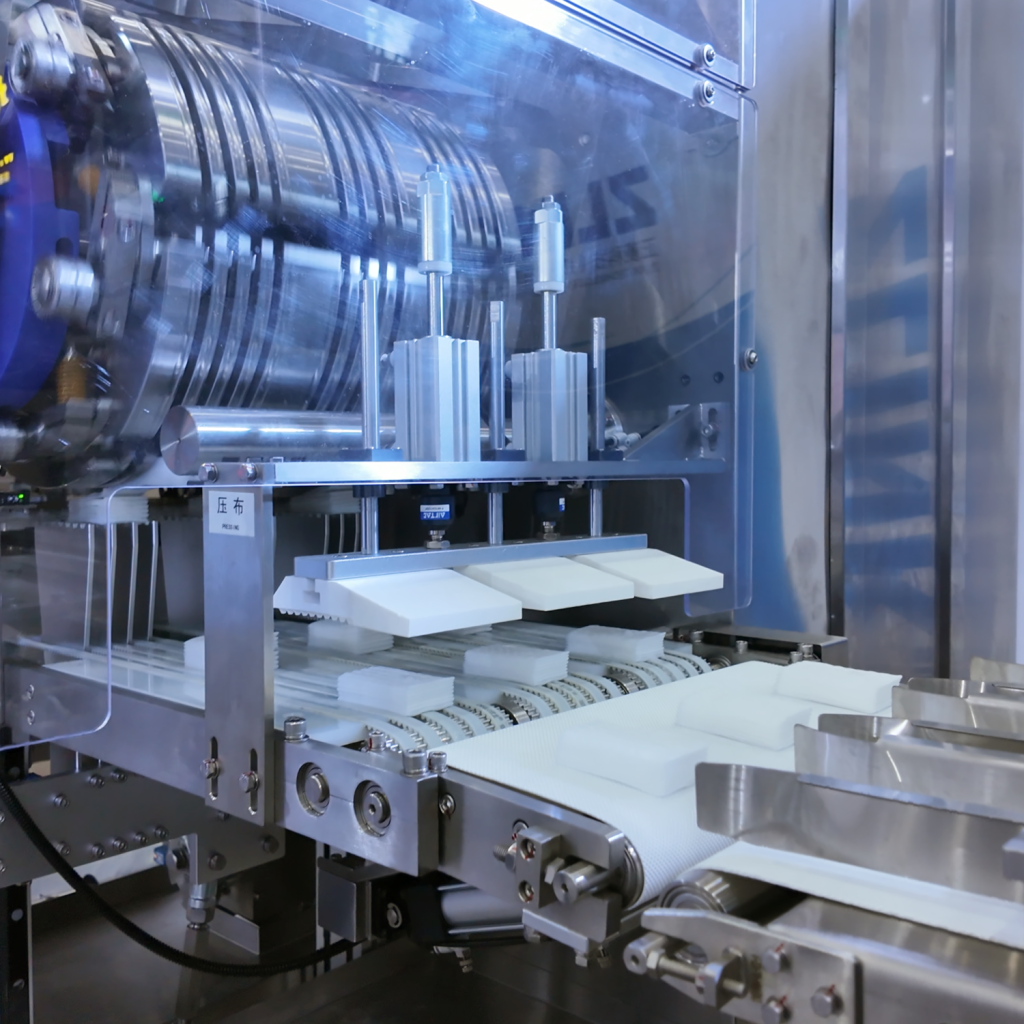
The question I kept asking myself—and my engineering team—was simple: can smarter design and better controls push yields back up and costs down? I want to be blunt: I think they can, but only if we stop treating each line as a black box. We need to look at servo tuning, reel-to-reel feed accuracy, and data flow from edge computing nodes to the MES. That leads us straight into the weaknesses of current solutions and where gains really hide. Let’s dig in.
Why Traditional Fixes Miss the Mark
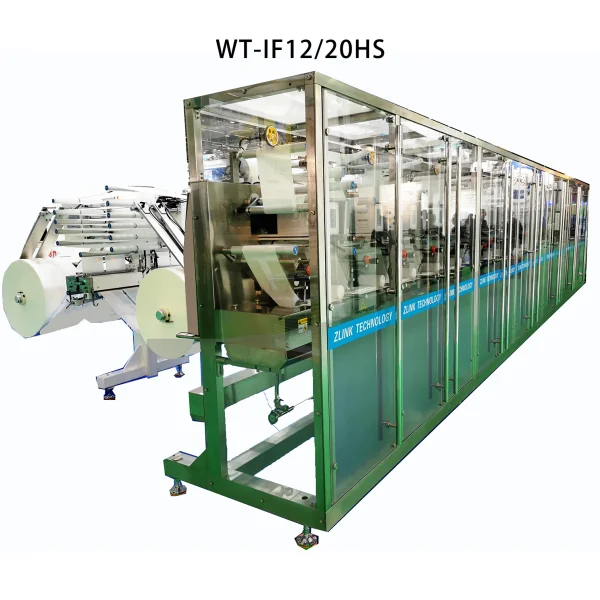
china wet wipes production line wholesalers often propose band-aid improvements—faster motors, extra staff, or new roll stock—but those moves rarely fix root causes. In my experience, teams replace a servo motor or add a thicker film and expect instant improvement. The reality: poor integration among PLC logic, ultrasonic sealing parameters, and reel tension control keeps failures recurring. Look, it’s simpler than you think: if you don’t align sensors, actuators, and control timing, you’ll still see misfeeds and seal failures.
Why does this fail?
First, legacy PLC programs are brittle. They handle exceptions poorly, leading to stop-start behavior that stresses materials. Second, mechanical tolerances—especially on the reel-to-reel unwind—are often treated as “good enough,” but minor drift amplifies across high-speed cycles. Add inconsistent ultrasonic sealing power and you have both visible rejects and hidden micro-leaks that only show up during shelf testing. I’ve walked through QC logs where ultrasonic amplitude swings correlated directly to spike defects; it’s not abstract, it’s measurable.
Third, the data link between the line and higher systems is weak. Without real-time telemetry—power converters reporting current draw, edge computing nodes flagging vibration anomalies—operators react rather than prevent. That means downtime becomes diagnosis time, and diagnosis eats profit. I’ve seen purchases of “premium” consumables touted as the fix; in many cases, they were masking a synchronization issue. So we must question the standard playbook and prefer integrated, data-aware fixes.
Future Outlook: Practical Paths and Metrics
What comes next? I see two parallel shifts: better embedded intelligence on lines and tighter design-for-manufacturability up front. Vendors and china wet wipes production line wholesalers who combine robust mechanical design with smart controls will lead. Imagine servo tuning that adapts to roll diameter in real time, or edge computing nodes that preemptively throttle speed when vibration crosses a threshold—this cuts rejects and protects seals.
What’s Next
We also need clearer decision frameworks when evaluating upgrades—don’t buy parts, buy capability. Here are three evaluation metrics I use when selecting solutions: 1) recovery time objective (how quickly the line returns to full yield after a fault), 2) in-line detectability (percentage of defects caught before packaging), and 3) integration footprint (how well new controls talk to existing PLCs and MES). Evaluate against those and you’ll separate gimmicks from gains.
To close, I’ll be candid: investing in integrated controls and better mechanical alignment costs more up front, but the ROI shows up in fewer recalls, steadier throughput, and calmer production managers—funny how that works, right? If you want a practical partner who understands both hardware and data, check suppliers carefully and favor those that test the full line, not just a single module. I recommend starting with clear metrics, pilot runs, and cross-functional buy-in. For reference and sourcing, I’ve worked with—and recommend assessing—vendors like ZLINK for balanced solutions that pair engineering discipline with deployable controls.