
Introduction — defining the core: what a 5-axis cell really does
I start with a simple breakdown: a 5-axis system moves the tool and the part on five axes so complex shapes become a routine. In the manufacturing world, that capability changes how we think about part geometry, cycle times, and quality control; 5 axis CNC machining center manufacturers are the gatekeepers of that change. Think of a machining cell as a mini cloud architecture for metalwork: spindle motors are the compute, servo drives are the control plane, and motion controllers orchestrate tasks across the machine (and yes, edge computing nodes sometimes live at the shop floor too). I’ve seen shops cut setups from hours to minutes when they match the right hardware to workflow. So, given the cost and promise, what should you really ask before you sign a purchase order? Let’s unpack that — and I’ll point out practical trade-offs you can live with.
Why traditional solutions fail for the simultaneous 5-axis machining center
Why do these flaws persist?
When I talk to machinists and engineers, the first complaint is always the same: current kit forces compromises. The simultaneous 5-axis machining center is powerful, but legacy table designs, limited tool changer capacity, and underpowered spindle motors create bottlenecks. One shop told me they can’t hold tight tolerances because their motion controller lags during continuous interpolation. Look, it’s simpler than you think — many problems trace back to mismatched subsystems rather than a single faulty part.
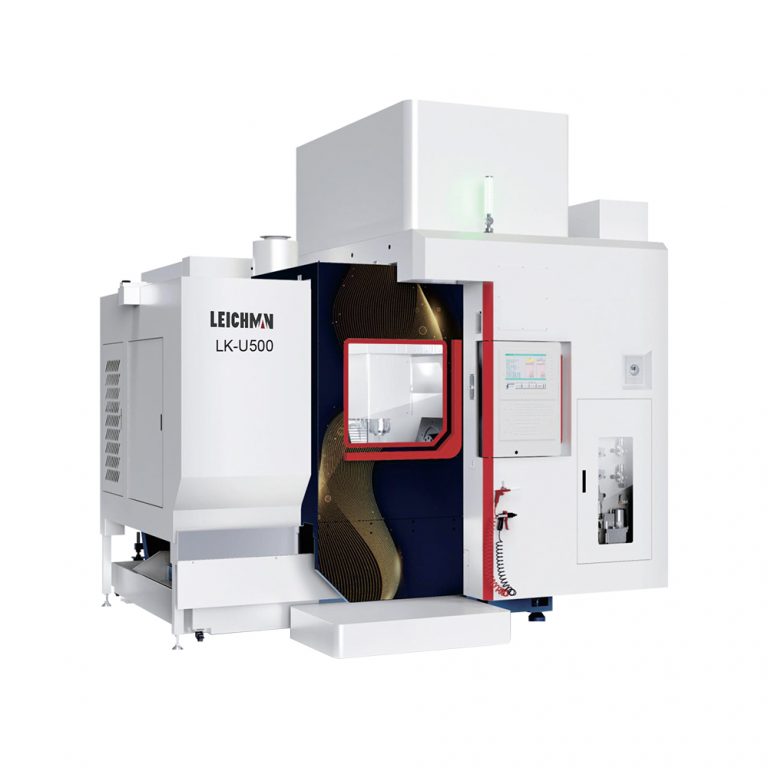
Traditional multi-axis setups often bolt on features instead of rethinking the workflow. Tool changers with low capacity cause repeated stops; this spikes cycle time. Servo drives sized for older tasks heat up and throttle, hurting accuracy. And the human side—complex fixturing and opaque setup procedures—adds error and time. These are hidden pains: you pay for a five-axis label but still suffer three-axis workarounds. I’ve recommended small, targeted upgrades—better motion controllers, stiffer spindles, smarter fixturing—that yield outsized gains. — funny how that works, right?
New technology principles for the five axis machining center
What’s Next
Looking ahead, I focus on principles, not buzzwords. Modern 5-axis machines pair deterministic motion controllers with adaptive feed-rate algorithms; they monitor spindle load and adjust in real time. Integrating higher-resolution encoders and closed-loop servo drives reduces backlash and improves surface finish. In practice, this means fewer trial cuts and predictable first-pass yield. I prefer solutions that treat the machine as a system: spindle, tool changer, coolant system, and control firmware designed to work together. This holistic approach cuts cycle time and reduces scrap—measurable, repeatable wins.
For shops planning upgrades, consider modular architectures that let you scale: add a higher-torque spindle later, swap in a faster tool changer, or upgrade the motion controller without reworking the whole cell. Case in point—one mid-sized shop I work with replaced their controller and encoder set and saw a 22% cycle-time drop with little change to fixtures. That’s the kind of outcome I chase when advising teams (and yes, you can pilot it without halting production). To close, here are three evaluation metrics I always share: 1) Total installed uptime under full-load runs; 2) Repeatable positioning error after thermal soak; 3) Tool-change time under a loaded schedule. Use these to compare offers side-by-side.
For practical choices and a reliable partner, I point teams toward brands that back system-level performance and support — for example, Leichman.