
Introduction — a shop story, a number, and a question
I once watched a small shop hustle to meet a late order while the old machine coughed and hiccupped—classic Friday chaos. A CNC turning and milling machine sat at the center of that storm, its control panel worn but still trusted. Recent industry reports show mid-sized shops with a 15–25% productivity gap when they mix legacy lathes and new cells (yes, that much). So I ask: how do we close that gap without burning cash or morale?
I want this piece to feel like a short talk over coffee. I’ll point out real problems I’ve seen on the floor, explain why some fixes fail, and then look ahead at smarter choices. Think of this as a practical map, not a sales pitch. Ready? Let’s move from the noise on the shop floor to the parts that actually matter.
Part 2 — Where the old fixes break down (a technical look)
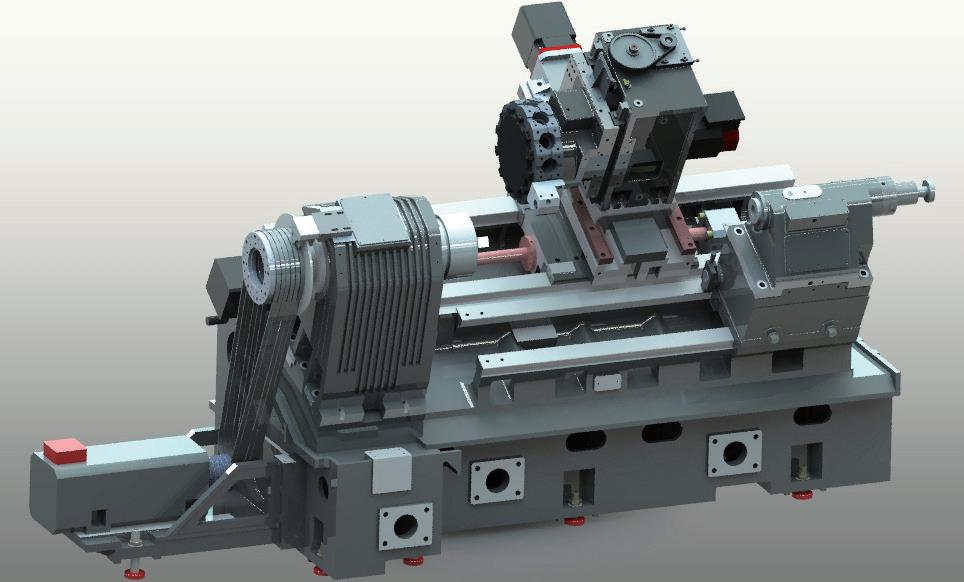
cnc heavy duty lathe — that phrase brings to mind strength and halves of a job done. But let me be blunt: heavy duty doesn’t always mean trouble-free. In many shops I visit, the obvious fix is to overload an old lathe with more work. That strains the spindle, confuses the CNC controller with mixed G-code styles, and forces us to babysit tool turret changes. I’ve seen shops chase uptime with band-aid schedules and more manual setup. It reduces short-term pain but creates long-term chaos.
What exactly breaks first?
Servo motors heat up. Bearings suffer. Precision slips. The result: scrap rates creep up. You think you’re saving time, but you’re losing parts and operator trust. Look, it’s simpler than you think—preventive maintenance and right-sized tooling matter more than just piling on hours. Also, older machines struggle when modern process demands lower tolerances and faster spindle speed changes. That friction costs hours and morale.
We must also face a hidden pain point: data mismatch. When a shop keeps machines on different control standards, the shop floor loses centralized insight. No consistent logging, no quick diagnostics—only guesswork and overtime. I’ve learned the hard way that retrofits without a systems plan just move the problem. — funny how that works, right? The takeaway: strong iron needs smart support—controls, spare parts, and clear procedures. Otherwise you buy horsepower and get headaches.
Part 3 — New principles and a forward-looking plan
Here’s where I shift from critique to construction. New technology principles matter: modular controls, edge computing nodes for local diagnostics, and better power converters that smooth motor torque. These are not buzzwords; they solve real shop problems. For instance, modular CNC controllers let you standardize G-code streams across cells. Edge nodes capture errors instantly and keep the network nimble. I’ve worked with teams that cut set-up time by half after adopting these ideas.
What’s Next — practical steps
Another practical path is service partnership. Use trusted providers for calibration and on-demand parts, and consider integrated options like cnc lathe machining services where offered. Real shops combine better hardware (tool turret upgrades, modern spindle drives) with smarter software and clear operator training. The result is steady cycle time, fewer crashes, and happier teams. — and yes, morale matters. It keeps people learning, not just firefighting.
To wrap up with actionable advice, here are three evaluation metrics I use when choosing upgrades or partners: 1) Mean time to restore (MTTR) — how fast will services get you back online? 2) Interoperability score — does the controller play nice with your MES and PLCs? 3) Total cost of ownership over five years — not just purchase price, but parts, downtime, and training. If a solution scores well on those three, I pay attention. If not, I walk away.
I’ve described problems, peeled back causes, and pointed to concrete improvements. I believe the best step you can take is honest assessment and steady upgrades, not dramatic overhauls. For teams ready to act, partners like Leichman can help bridge the gap between old iron and modern workflows.